
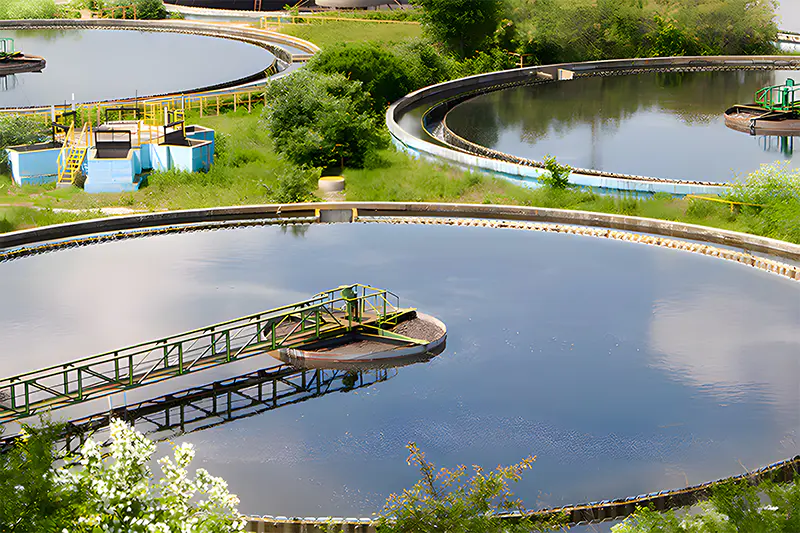
Industrial growth and municipal expansion create continuous pressure on freshwater supplies across the globe. Modern facility managers increasingly rely on scientific breakthroughs to purify impaired sources and reclaim wastewater effectively. Reverse osmosis technology provides a reliable scientific framework for separating dissolved minerals and contaminants from aqueous solutions. Implementing these physical separation techniques allows industries to recover valuable liquid streams and minimize their discharge volumes.
Fundamentals of Pressure Driven Filtration
Pressure-driven membrane processes rely on specialized semi-permeable barriers to filter dissolved solutes from aqueous feeds. Reverse osmosis technology operates by applying an external hydraulic force that overcomes natural osmotic equilibrium. Microscopic pores block unwanted ionic species while letting pure solvent molecules flow through smoothly.
Specialized thin-film composite materials maximize both permeability and salt rejection performance during continuous industrial running hours. Proper pretreatment steps remain critical for preventing membrane fouling, particulate scaling, and biological degradation in complex setups.
Expanding Applications in Municipal Seawater Desalination
Coastal municipalities frequently look to the world’s oceans to supplement dwindling surface water and groundwater reserves. Reverse osmosis technology significantly lowers power consumption compared to older thermal distillation methods used in past decades. Modern element geometries optimize fluid dynamics to maximize freshwater yield while reducing operating pressure demands.
Regional water authorities utilize multi-stage system configurations to process saline water sources containing diverse chemical contaminants. These integrated systems consistently remove heavy minerals and trace organics without introducing harmful chemical agents into the environment.
Industrial Wastewater Reclamation and Reuse Strategies
Factories generate large volumes of liquid effluent that require intensive treatment before safe discharge or internal recycling. Reverse osmosis technology facilitates closed-loop water cycles within chemical manufacturing plants and power generation stations. Water treatment membrane technology plays a vital role in wastewater reuse projects by removing suspended solids, colloids, and dissolved salts so that liquid recycling can be successfully achieved.
Advanced reclamation projects depend heavily on robust pretreatment trains incorporating ultrafiltration or nanofiltration units. Upstream filtration barriers protect sensitive separation surfaces from particulate clogging and sudden chemical damage.
Economic Advantages and Resource Optimization
Adopting advanced separation systems yields substantial financial savings for large-scale industrial operations over extended operating periods. Reduced chemical consumption and lower energy demands translate directly into decreased operational expenditures for facility owners. Furthermore, minimizing freshwater withdrawal mitigates business risks associated with regional scarcity and rising municipal utility tariffs.
Sustainable industrial practices require careful management of liquid waste streams and concentrated brine byproducts. Optimizing recovery rates helps operations comply with environmental regulations while preserving surrounding natural aquatic ecosystems.
Addressing Operational Challenges and Maintenance Protocols
Membrane longevity depends heavily on proactive maintenance schedules and systematic chemical cleaning regimens. Scaling caused by calcium sulfate or silica threatens system performance if specialized antiscalants are not precisely dosed. Plant operators monitor normalized permeate flow and salt passage daily to detect early signs of performance decline.
Biological fouling presents another persistent challenge in reuse operations where nutrient levels remain elevated. Periodic clean-in-place procedures utilizing approved cleaning formulations restore membrane flux safely and effectively. Implementing predictive analytics to track flux decline and differential pressure trends allows operators to shift from reactive to proactive maintenance, minimizing unplanned downtime and optimizing chemical usage over the membrane’s lifecycle.
Advancements in High Purity Water Preparation
High-purity water requirements demand exceptionally rigorous filtration standards across modern electronics and pharmaceutical manufacturing facilities. In the high-purity water project, water treatment membrane technology is mainly used for the preparation of ultrapure water in the electronics, pharmaceutical and other industries. Reverse osmosis membrane (RO) and electrodeionisation (EDI) technologies are key technologies in high purity water preparation, as they can effectively remove ions, organics and micro-organisms from water to ensure that the water quality reaches the required purity.
Specialized polishing procedures, such as mixed-bed ion exchange, further purify the liquid to meet strict specifications. The application of these methods enables high-purity water projects to meet the needs of sensitive high-end technological production.
Environmental Impact and Sustainability Goals
Water treatment infrastructure plays a critical role in global environmental protection and resource conservation initiatives. Effective recycling projects drastically reduce the volume of industrial effluent discharged into local natural waterways. Lowering operational energy footprints aligns industrial expansion with broader ecological sustainability objectives.
Preserving natural water bodies requires continuous technical innovation and rigorous operational management. Modern membrane systems bridge the gap between industrial productivity and ecological responsibility. By integrating real-time monitoring and adaptive control technologies, these systems not only minimize chemical usage but also enhance water recovery rates, further advancing the transition toward a circular economy.
Conclusion
Industrial water management continues to evolve as global demand for clean resources intensifies. Reverse osmosis technology provides a scientifically proven framework for desalination, purification, and wastewater reclamation. Runmo manufactures high-performance industrial membranes designed to address rigorous filtration challenges across diverse sectors.
Runmo supplies specialized components such as the BW series for brackish water desalination and the SW series for demanding seawater applications, helping engineers achieve sustainable, cost-effective water treatment outcomes. Contact the specialist team today to discuss specific project requirements.
